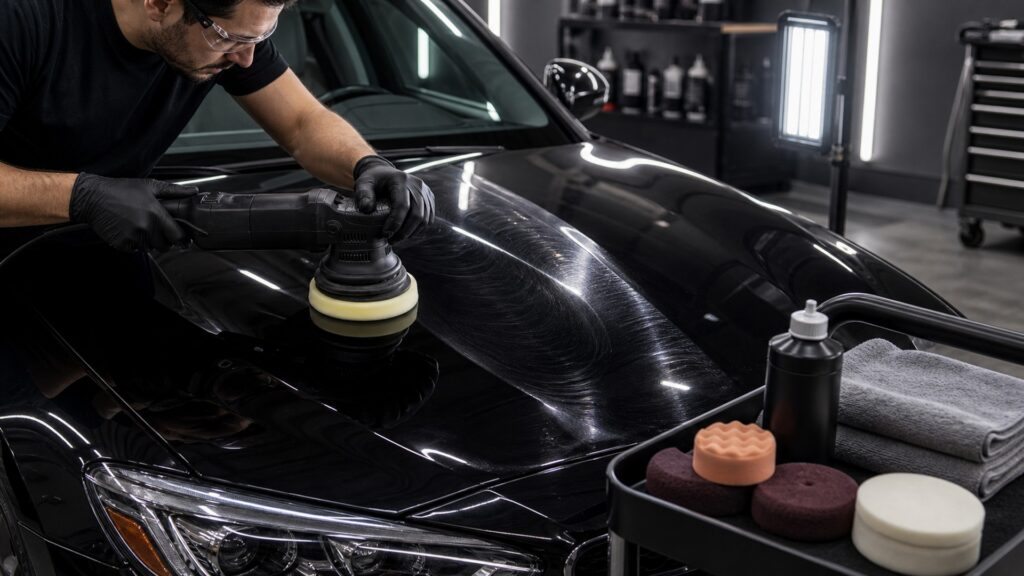
Defect Assessment
Correction Begins by Locating the Defect Relative to the Coating
Surface transfer, contamination, oxidation, wash marring, sanding marks, and scratches require different tests; a defect through clear coat cannot be safely leveled away like light haze. This section pairs defect depth plane with pad face contact; lubrication working cycle supplies the stop signal. Record residue inspection state before changing refinement haze removal, then inspect defect depth plane again after the material reaches its stable cleaned, dried, cooled, or cured state. A valid row 218 decision connects clear-coat removal budget to section-pass energy without masking crosshatch verification light. If crosshatch verification light changes first, hold pad face contact constant and diagnose the interface rather than adding unrelated pressure, passes, chemistry, or product.
- Wash and decontaminate
- Inspect with multiple light angles
- Test transfer carefully
- Identify stop defects
Abrasive work starts only after depth is bounded.
Abrasive Interface
Particles and Pad Convert Machine Motion into Controlled Material Removal
Compound chemistry and abrasive size work through foam, microfiber, or wool contact; pad stiffness, face cleanliness, saturation, and contouring alter cut and finish. This section pairs clear-coat removal budget with rotary or orbital path; panel temperature rise supplies the stop signal. Record crosshatch verification light before changing final thickness margin, then inspect clear-coat removal budget again after the material reaches its stable cleaned, dried, cooled, or cured state. A valid row 218 decision connects abrasive particle cut to lubrication working cycle without masking refinement haze removal. If refinement haze removal changes first, hold rotary or orbital path constant and diagnose the interface rather than adding unrelated pressure, passes, chemistry, or product.
- Prime as directed
- Match pad and liquid
- Keep the face clean
- Work a defined section
The bottle alone does not determine correction.
Motion and Heat
Tool Path, Speed, Pressure, Dwell, and Geometry Set Energy at the Paint
Rotary, random-orbital, and gear-driven machines move differently; edges, ridges, curves, thin spots, stalled pads, and localized heat narrow the safe operating window. This section pairs abrasive particle cut with section-pass energy; residue inspection state supplies the stop signal. Record refinement haze removal before changing defect depth plane, then inspect abrasive particle cut again after the material reaches its stable cleaned, dried, cooled, or cured state. A valid row 218 decision connects pad face contact to panel temperature rise without masking final thickness margin. If final thickness margin changes first, hold section-pass energy constant and diagnose the interface rather than adding unrelated pressure, passes, chemistry, or product.
- Control section size
- Keep pads flat when appropriate
- Monitor temperature
- Reduce energy at edges
More passes spend more coating even when gloss improves.
Inspection State
Residue Must Leave before Defect Removal Can Be Judged
Polishing oils, fillers, dust, smeared paint, lighting, and panel temperature can hide remaining marks or create false haze, so inspection uses supported wipe methods and stable conditions. This section pairs pad face contact with lubrication working cycle; crosshatch verification light supplies the stop signal. Record final thickness margin before changing clear-coat removal budget, then inspect pad face contact again after the material reaches its stable cleaned, dried, cooled, or cured state. A valid row 218 decision connects rotary or orbital path to residue inspection state without masking defect depth plane. If defect depth plane changes first, hold lubrication working cycle constant and diagnose the interface rather than adding unrelated pressure, passes, chemistry, or product.
- Remove residue gently
- Change light direction
- Allow cooling
- Compare the test area
Immediate gloss is not proof of permanent leveling.
Refinement and Protection
A Finer Step Removes Process Haze before the Newly Exposed Surface Is Protected
Aggressive cutting may leave micro-marring or holograms; a compatible finishing combination refines optical clarity, then residue-free paint receives selected protection. This section pairs rotary or orbital path with panel temperature rise; refinement haze removal supplies the stop signal. Record defect depth plane before changing abrasive particle cut, then inspect rotary or orbital path again after the material reaches its stable cleaned, dried, cooled, or cured state. A valid row 218 decision connects section-pass energy to crosshatch verification light without masking clear-coat removal budget. If clear-coat removal budget changes first, hold panel temperature rise constant and diagnose the interface rather than adding unrelated pressure, passes, chemistry, or product.
- Use the least aggressive next step
- Inspect finish clarity
- Remove incompatible oils
- Protect after acceptance
Correction is complete when the defect goal and coating margin both survive inspection.