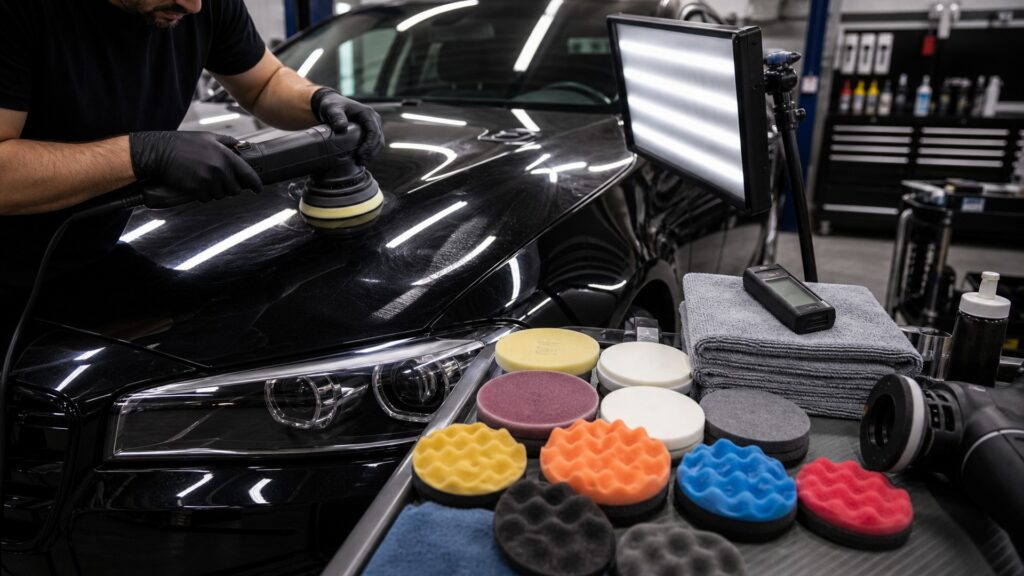
Why Polishing & Paint Correction Fitment Matters

Paint-correction fitment matters because the same mark can be removable transfer, bonded contamination, oxidation, clear-coat marring, a deep scratch, repaint texture, cracking, or failure below the surface. Each has a different safe response, and some should not be polished at all.

The workable system joins paint evidence to tool movement, pad material and size, abrasive, section technique, environment, skill, inspection, and the owner's finish goal. A successful test spot is a local compatibility result—not permission to repeat the same energy across thin edges, repaired panels, curves, or different paint.

By: Review Streets Research Lab
Updated: September 1, 2026
Explainer · 8-12 min read
polishing & paint correction fitment explainer hero image for Review Streets
What You'll Learn

Resolve Polishing and Paint Correction Fitment through Its Controlling Evidence

Fitment joins a mapped defect to the remaining paint, local geometry, one abrasive interface, and a finish target that preserves a defensible coating margin.

  • The Method Must Match What the Mark Actually Is
  • Hardness, Thickness, Repair, Age, and Failure Change the Available Margin
  • Tool Motion, Backing Plate, Pad, Abrasive, and Section Technique Work as One Combination
  • Temperature, Lighting, Power, Ventilation, Space, and Cleanliness Affect Control
  • Residual Defect, Coating Margin, Time, Cost, and Future Protection Need an Explicit Tradeoff
  • How to verify the finished state

Tip: Treat every panel transition as a new local case; repeat the test logic, not blindly the same speed, pad, pressure, or pass count.

Definitions

Key Concepts That Define Polishing and Paint Correction Fitment

These terms identify the evidence that authorizes, limits, or stops irreversible leveling on a particular area of painted bodywork.

Defect Classification

Defect Classification locates the interface where polishing and paint correction fitment under the named surface and operating conditions.

  • Measure defect classification before work
  • Observe how defect classification changes
  • Record defect classification after verification

Paint-System Hardness

Paint-System Hardness sets the usable boundary for polishing and paint correction fitment under the named surface and operating conditions.

  • Measure paint-system hardness before work
  • Observe how paint-system hardness changes
  • Record paint-system hardness after verification

Film-Build Evidence

Film-Build Evidence explains the material response during polishing and paint correction fitment under the named surface and operating conditions.

  • Measure film-build evidence before work
  • Observe how film-build evidence changes
  • Record film-build evidence after verification

Repaint History

Repaint History measures the transfer created by polishing and paint correction fitment under the named surface and operating conditions.

  • Measure repaint history before work
  • Observe how repaint history changes
  • Record repaint history after verification

Edge And Ridge Geometry

Edge And Ridge Geometry reveals the failure condition within polishing and paint correction fitment under the named surface and operating conditions.

  • Measure edge and ridge geometry before work
  • Observe how edge and ridge geometry changes
  • Record edge and ridge geometry after verification

Machine Orbit Or Rotation

Machine Orbit Or Rotation records the verified outcome after polishing and paint correction fitment under the named surface and operating conditions.

  • Measure machine orbit or rotation before work
  • Observe how machine orbit or rotation changes
  • Record machine orbit or rotation after verification

Tip: Record paint history and geometry beside the test result so a central-panel success is never generalized to an edge or repair.

Defect Fit

The Method Must Match What the Mark Actually Is

Cleaning removes soil, decontamination removes bonded material, correction levels selected surface defects, and refinishing addresses damage beyond a safe abrasive margin. This section pairs defect classification with repaint history; pad diameter and material supplies the stop signal. Record temperature and lighting control before changing acceptable residual defect, then inspect defect classification again after the material reaches its stable cleaned, dried, cooled, or cured state. A valid row 219 decision connects paint-system hardness to machine orbit or rotation without masking operator test-spot repeatability. If operator test-spot repeatability changes first, hold repaint history constant and diagnose the interface rather than adding unrelated pressure, passes, chemistry, or product. Fitment trial 1 begins with defect classification and the local panel history, then changes only one member of the abrasive system while film-build evidence and edge and ridge geometry stay fixed. The cooled, residue-free reading of pad diameter and material is compared with temperature and lighting control, because a gloss change without a stable defect response cannot authorize repetition. The panel map separately marks edges, ridges, repairs, small curves, substrate changes, and inaccessible readings around repaint history. Those zones receive their own abrasive cut profile limit; if acceptable residual defect cannot be demonstrated there, the accepted plan leaves the defect, changes technique, or refers refinishing instead of copying the central-panel test.

  • Classify before cutting
  • Check multiple light angles
  • Distinguish transfer from depth
  • Define acceptance

Misclassification spends coating without solving the cause.

Paint Fit

Hardness, Thickness, Repair, Age, and Failure Change the Available Margin

Original and repainted panels can respond differently; thin, checked, lifting, burned, matte, or unknown coatings impose strong stop conditions. This section pairs paint-system hardness with edge and ridge geometry; abrasive cut profile supplies the stop signal. Record operator test-spot repeatability before changing post-correction protection, then inspect paint-system hardness again after the material reaches its stable cleaned, dried, cooled, or cured state. A valid row 219 decision connects film-build evidence to pad diameter and material without masking acceptable residual defect. If acceptable residual defect changes first, hold edge and ridge geometry constant and diagnose the interface rather than adding unrelated pressure, passes, chemistry, or product. Fitment trial 2 begins with paint-system hardness and the local panel history, then changes only one member of the abrasive system while repaint history and machine orbit or rotation stay fixed. The cooled, residue-free reading of abrasive cut profile is compared with operator test-spot repeatability, because a gloss change without a stable defect response cannot authorize repetition. The panel map separately marks edges, ridges, repairs, small curves, substrate changes, and inaccessible readings around edge and ridge geometry. Those zones receive their own temperature and lighting control limit; if post-correction protection cannot be demonstrated there, the accepted plan leaves the defect, changes technique, or refers refinishing instead of copying the central-panel test.

  • Map panel history
  • Measure when appropriate
  • Inspect edges and ridges
  • Avoid unstable paint

Correction capacity belongs to the paint, not the machine.

System Fit

Tool Motion, Backing Plate, Pad, Abrasive, and Section Technique Work as One Combination

Rotary, random-orbital, and gear-driven paths create different contact behavior; pad size, foam, fiber, wool, cut, lubrication, pressure, and passes tune the result. This section pairs film-build evidence with machine orbit or rotation; temperature and lighting control supplies the stop signal. Record acceptable residual defect before changing defect classification, then inspect film-build evidence again after the material reaches its stable cleaned, dried, cooled, or cured state. A valid row 219 decision connects repaint history to abrasive cut profile without masking post-correction protection. If post-correction protection changes first, hold machine orbit or rotation constant and diagnose the interface rather than adding unrelated pressure, passes, chemistry, or product. Fitment trial 3 begins with film-build evidence and the local panel history, then changes only one member of the abrasive system while edge and ridge geometry and pad diameter and material stay fixed. The cooled, residue-free reading of temperature and lighting control is compared with acceptable residual defect, because a gloss change without a stable defect response cannot authorize repetition. The panel map separately marks edges, ridges, repairs, small curves, substrate changes, and inaccessible readings around machine orbit or rotation. Those zones receive their own operator test-spot repeatability limit; if defect classification cannot be demonstrated there, the accepted plan leaves the defect, changes technique, or refers refinishing instead of copying the central-panel test.

  • Start with a test spot
  • Use supported combinations
  • Keep pads serviceable
  • Document settings

Changing one component changes the whole interface.

Environment Fit

Temperature, Lighting, Power, Ventilation, Space, and Cleanliness Affect Control

Heat changes working cycles and paint response; weak light hides defects; dust contaminates pads; cords, hoses, noise, and residue create safety and quality constraints. This section pairs repaint history with pad diameter and material; operator test-spot repeatability supplies the stop signal. Record post-correction protection before changing paint-system hardness, then inspect repaint history again after the material reaches its stable cleaned, dried, cooled, or cured state. A valid row 219 decision connects edge and ridge geometry to temperature and lighting control without masking defect classification. If defect classification changes first, hold pad diameter and material constant and diagnose the interface rather than adding unrelated pressure, passes, chemistry, or product. Fitment trial 4 begins with repaint history and the local panel history, then changes only one member of the abrasive system while machine orbit or rotation and abrasive cut profile stay fixed. The cooled, residue-free reading of operator test-spot repeatability is compared with post-correction protection, because a gloss change without a stable defect response cannot authorize repetition. The panel map separately marks edges, ridges, repairs, small curves, substrate changes, and inaccessible readings around pad diameter and material. Those zones receive their own acceptable residual defect limit; if paint-system hardness cannot be demonstrated there, the accepted plan leaves the defect, changes technique, or refers refinishing instead of copying the central-panel test.

  • Stabilize panel temperature
  • Use cross-lighting
  • Route power safely
  • Keep work clean

An uncontrolled bay can invalidate a good combination.

Goal Fit

Residual Defect, Coating Margin, Time, Cost, and Future Protection Need an Explicit Tradeoff

Preserving paint may require leaving deeper marks; show-car refinement, daily-driver improvement, isolated repair, and sale preparation justify different endpoints. This section pairs edge and ridge geometry with abrasive cut profile; acceptable residual defect supplies the stop signal. Record defect classification before changing film-build evidence, then inspect edge and ridge geometry again after the material reaches its stable cleaned, dried, cooled, or cured state. A valid row 219 decision connects machine orbit or rotation to operator test-spot repeatability without masking paint-system hardness. If paint-system hardness changes first, hold abrasive cut profile constant and diagnose the interface rather than adding unrelated pressure, passes, chemistry, or product. Fitment trial 5 begins with edge and ridge geometry and the local panel history, then changes only one member of the abrasive system while pad diameter and material and temperature and lighting control stay fixed. The cooled, residue-free reading of acceptable residual defect is compared with defect classification, because a gloss change without a stable defect response cannot authorize repetition. The panel map separately marks edges, ridges, repairs, small curves, substrate changes, and inaccessible readings around abrasive cut profile. Those zones receive their own post-correction protection limit; if film-build evidence cannot be demonstrated there, the accepted plan leaves the defect, changes technique, or refers refinishing instead of copying the central-panel test.

  • Set the finish target
  • Prioritize coating preservation
  • Agree on residual defects
  • Plan protection

Maximum defect removal is not automatically the best fit.

Quick Reality Check

Where Polishing and Paint Correction Fitment Helps—and Where It Stops

A correction system fits only where defect evidence, coating reserve, geometry, operator control, and inspection all support the same bounded result.

Evidence That the Local Paint Accepts Correction

defect classification and paint-system hardness remain controlled while film-build evidence produces the expected material response.

repaint history, edge and ridge geometry, and machine orbit or rotation can be observed independently without masking residue or an unstable finish.

Evidence That Narrows or Ends the Test

Stop when pad diameter and material, abrasive cut profile, or temperature and lighting control cannot be verified within the supported process window.

Unknown material, uncontrolled operator test-spot repeatability, incompatible acceptable residual defect, or failed post-correction protection requires another method, location, repair, or qualified service.

Common Myths

Misconceptions About Polishing and Paint Correction Fitment

Correction myths promote a convenient product or reading above the physical margin of the paint being altered.

A paint-depth reading makes every area safe

A reading has instrument, substrate, layer, geometry, calibration, and access limits; edges, ridges, repairs, prior sanding, and coating failure still require conservative judgment. Verify polishing and paint correction fitment on the named material after complete drying.

Soft paint always needs a softer pad

Paint response comes from the whole abrasive, pad, machine, pressure, speed, dwell, residue, and heat system; a simplistic hardness-to-pad rule can haze or under-correct. Check polishing and paint correction fitment against vehicle guidance and the observed residue.

The test spot can be copied unchanged to every panel

Panels differ in material, repair history, thickness, curvature, temperature, defect load, access, and edge exposure, so the test process must be revalidated across changed conditions. Confirm polishing and paint correction fitment with a controlled test before broader application.

Perfect correction is the correct goal

Chasing every deep mark can consume unnecessary clear coat and create edge or heat damage; an acceptable residual defect may preserve far more long-term paint integrity. Reinspect polishing and paint correction fitment under stable light, temperature, and moisture conditions.

Tip: Challenge the shortcut with a clean test area, controlled variables, stable temperature, residue-free inspection, and an explicit stop rule.

FAQ

Frequently Asked Questions About Polishing and Paint Correction Fitment

These answers cover conservative escalation, machine movement, high-risk panel zones, abort conditions, and final residue-free acceptance.

How is the least aggressive method found?

After washing and decontamination, test a conservative supported abrasive, pad, tool, and technique on a representative area, inspect clean, then escalate one variable deliberately. Document polishing and paint correction fitment, the affected surface, and the final functional check.

Does machine type determine safety?

No. Rotary, random-orbital, and gear-driven tools each require compatible pads, abrasives, technique, geometry control, temperature management, and operator competence. Keep polishing and paint correction fitment within the product label and recovery capacity.

What panel areas need extra caution?

Edges, ridges, body lines, thin spots, repaints, small curves, plastic panels, damaged clear coat, taped boundaries, adjacent trim, and restricted access narrow the margin. Judge polishing and paint correction fitment by transferred soil rather than immediate appearance.

When should polishing stop?

Stop for rising heat, unstable paint, color transfer suggesting unexpected layers, pad contamination, tool faults, poor visibility, uncertain thickness, excessive residue, or no controlled improvement. Stop polishing and paint correction fitment when color, texture, grip, or adhesion changes.

How is the final fit verified?

Inspect the clean cooled surface under multiple lights, confirm the agreed defect reduction and finish, document residual defects, preserve coating margin, and apply compatible protection. Compare polishing and paint correction fitment with the untreated area after all residue leaves.

Bottom Line

Why Polishing & Paint Correction Fitment Matters turns on defect classification, paint-system hardness, and film-build evidence; the decision remains incomplete until repaint history, edge and ridge geometry, and machine orbit or rotation are documented.

Accept the result only when pad diameter and material, abrasive cut profile, and temperature and lighting control remain compatible with operator test-spot repeatability, acceptable residual defect, and post-correction protection after the applicable inspection interval.

Next Steps

Continue the Polishing and Paint Correction Fitment Decision

Continue with the material-removal mechanism, the wash boundary that precedes it, and the separate fitment of protection after refinement.

Quick Summary

Polishing and Paint Correction Fitment Explained

  • The Method Must Match What the Mark Actually Is
  • Hardness, Thickness, Repair, Age, and Failure Change the Available Margin
  • Tool Motion, Backing Plate, Pad, Abrasive, and Section Technique Work as One Combination
  • Temperature, Lighting, Power, Ventilation, Space, and Cleanliness Affect Control
  • Residual Defect, Coating Margin, Time, Cost, and Future Protection Need an Explicit Tradeoff